Mining buyers demand more than machine power
By admin September 1, 2026 5:35 pm IST
As mining operations become larger and more demanding, equipment buyers are placing greater emphasis on productivity, durability and lifecycle efficiency when selecting excavators.
What excavator attributes matter most for overburden removal and high-tonnage mining applications?
Customers look for excavators that deliver consistent productivity under demanding conditions while maintaining low operating costs. The most critical attributes include high breakout force, faster cycle times, hydraulic efficiency, structural durability, operating stability, bucket capacity, and ease of maintenance. Since mining equipment operates continuously in abrasive environments, reliability, fuel efficiency, and operator comfort are equally important for maximising machine availability and site productivity.
These priorities are reflected in excavators engineered for demanding mining operations. The CASE CX220C LC, for instance, features the CASE Intelligent Hydraulic System (CIHS), which optimises hydraulic performance to deliver faster response, efficient digging, and lower fuel consumption. Its reinforced boom and arm, robust undercarriage, and balanced design provide the durability and stability required for handling high material volumes in mining and quarry applications. Simplified service access and an ergonomic operator cabin further help reduce maintenance time and operator fatigue.
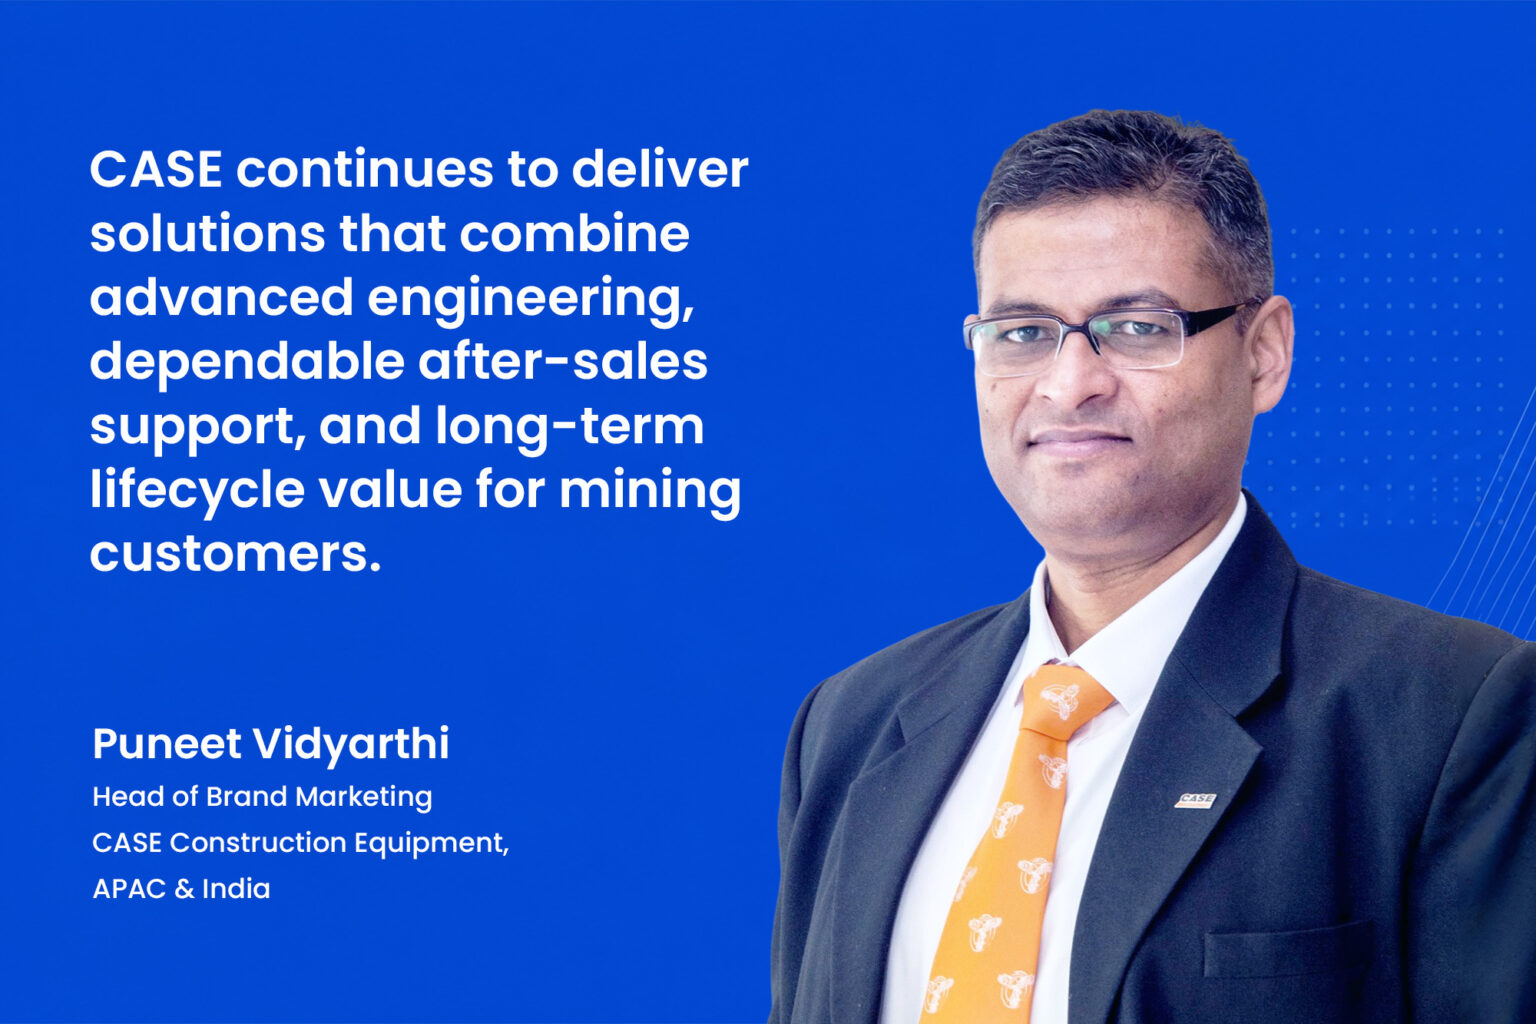
As India’s mining sector expands through commercial mining reforms and the National Critical Mineral Mission, CASE continues to deliver solutions that combine advanced engineering, dependable after-sales support, and long-term lifecycle value for mining customers.
How is myCASE telematics helping mining customers manage uptime and maintenance across large fleets?
As mining operations become larger and more production-driven, fleet visibility is becoming as important as machine performance. Customers require real-time insights to improve equipment availability, plan maintenance and optimise fleet utilisation across multiple sites. Digital fleet management is therefore becoming an integral part of modern mining operations.
We address this need through myCASE Construction, its telematics platform that enables customers to monitor machine health and performance remotely. The system provides information on machine location, operating hours, fuel consumption, idle time, fault alerts and service intervals, helping fleet managers make informed operational decisions. By identifying potential maintenance requirements before they lead to unplanned breakdowns, myCASE supports proactive maintenance planning, helping reduce downtime and improve machine availability. It also supports more efficient service scheduling, equipment deployment and fleet utilisation.
As mining companies increasingly adopt data-driven asset management, telematics has evolved from a value-added feature into an important operational tool. Through myCASE Construction, CASE helps customers improve fleet productivity, support equipment life and make maintenance planning more predictable, while contributing to lower lifecycle costs.

What procurement factors are most critical when mining companies choose between standard and long-carriage excavator configurations?
In mining and quarry operations, undercarriage durability and traction are important considerations because equipment often works on uneven, rocky and abrasive terrain. Procurement teams therefore assess ground conditions, material characteristics, machine mobility, excavation and loading requirements, and the level of stability required before selecting a suitable configuration. The durability and design of the undercarriage are also important considerations for equipment expected to operate in demanding conditions.
The choice between standard and long-carriage excavators is consequently driven by the specific application rather than a one-size-fits-all approach. The CASE CX220C provides an example of this application-focused approach. Its specifications include a reinforced guide frame for the LC version, while 700 mm triple-grouser steel shoes are available as an LC-specific option. These options give customers greater flexibility when specifying the machine for different operating requirements.
We work with customers to understand site-specific conditions and recommend equipment suited to their operational requirements. As mining projects become more specialised, procurement decisions are increasingly focused on application suitability, operational efficiency and long-term value.
How are BS (CEV) Stage V emission norms changing the specifications mining equipment buyers look for?
The implementation of BS (CEV) Stage V emission norms has significantly influenced how mining companies evaluate new equipment. While compliance with the latest emission standards is a prerequisite, customers are increasingly looking beyond regulatory requirements to assess how advanced engine technologies affect fuel efficiency, machine performance, serviceability, and long-term operating costs. Buyers also expect equipment that delivers these environmental benefits without compromising productivity or reliability in demanding mining conditions.
BS (CEV) Stage V-compliant machines are designed to meet these evolving expectations by integrating advanced engine and emission-control technologies that support lower emissions while maintaining dependable performance. Alongside regulatory compliance, CASE continues to focus on fuel efficiency, operator productivity, and ease of maintenance to help customers achieve consistent performance in challenging mining applications. This balanced approach enables mining companies to align sustainability objectives with operational efficiency.
With the Government of India progressively strengthening emission standards for construction equipment, equipment selection is increasingly influenced by environmental compliance alongside operational performance. CASE is supporting this transition by offering machines that combine regulatory compliance with engineering solutions tailored to the productivity and reliability requirements of India’s mining sector.
What has changed in customer expectations around total cost of ownership for mining equipment fleets?
Mining customers are increasingly looking beyond the initial purchase price when evaluating equipment. Factors such as local manufacturing, parts availability, service response, maintenance predictability, component life and equipment uptime now play a significant role in determining the total cost of ownership and long-term fleet value.
CASE India is addressing these expectations through its manufacturing and aftermarket ecosystem in India. Our Pithampur facility supports the Indian market and export markets, while the company continues to strengthen local manufacturing and localisation capabilities. We also support parts availability through our logistics network, including a central warehouse in Indore and depots in Faridabad and Guwahati, helping improve supply-chain responsiveness. In addition, its FLEETPro range of value-based replacement parts provides maintenance solutions for ageing equipment and mature fleets.
This is complemented by genuine CASE parts, dealer and service support, and programmes such as CASE Care, which focus on proactive maintenance and reducing downtime. Aligned with the Government of India’s Make in India initiative, CASE continues to strengthen its local manufacturing and aftermarket ecosystem. For mining customers, these capabilities contribute to improved equipment availability, faster service response and greater cost predictability throughout the machine’s operating life. The shift in expectations is clear: customers increasingly want an equipment partner that delivers measurable lifecycle value and dependable long-term fleet support, rather than simply supplying a machine at the point of purchase.